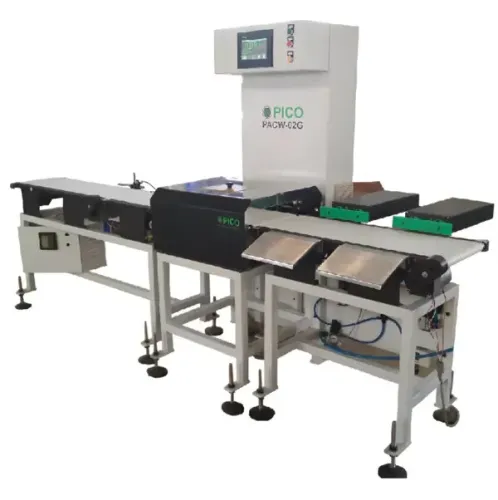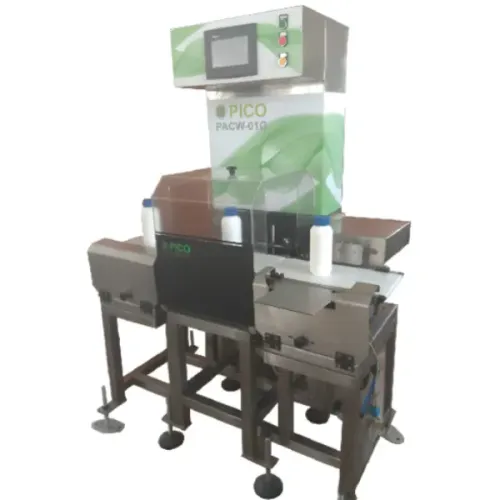
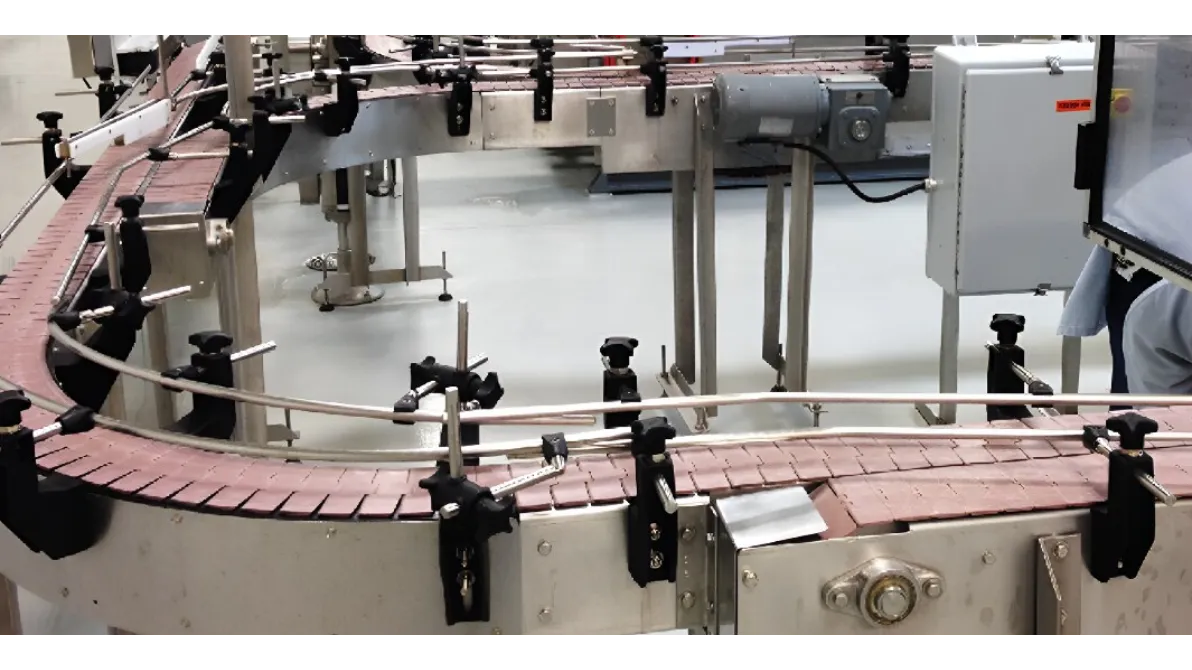
Efficient movement of raw materials, components, and finished products is essential for maintaining consistent production. Whether operating a manufacturing plant, packaging facility, warehouse, or logistics center, businesses rely on well-designed Industrial Material Handling Conveyor Solutions to improve productivity while reducing manual effort.
Modern conveyor systems are no longer limited to transporting products from one point to another. They now play an important role in automation, inventory management, production synchronization, and workplace safety. For industries in Coimbatore, Tamil Nadu, adopting the right material handling solution can significantly improve operational performance.
Why Material Handling Matters
Every manufacturing process depends on smooth material flow.
When products move inefficiently between workstations, businesses often experience:
- Production delays
- Increased labor costs
- Product damage
- Inventory congestion
- Workflow interruptions
- Lower equipment utilization
A properly designed conveyor system eliminates many of these challenges by creating a continuous and organized production process.
Types of Industrial Material Handling Conveyors
Different industries require different conveyor systems depending on product characteristics and production requirements.
Some commonly used solutions include:
Belt Conveyors
Ideal for transporting packaged goods, lightweight materials, and finished products.
Roller Conveyors
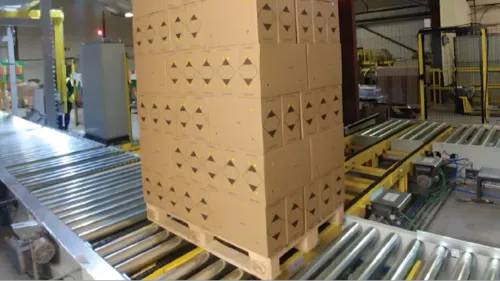
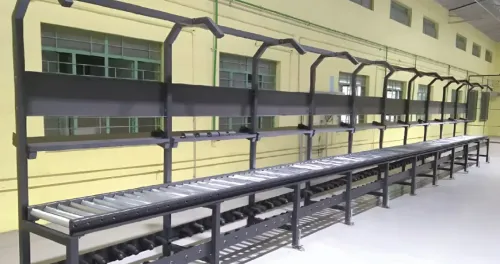
Suitable for cartons, pallets, crates, and warehouse logistics operations.
Chain Conveyors
Designed for moving heavy industrial loads with stability and durability.
Inclined Conveyors
Used to transfer products between different production levels while optimizing floor space.
Modular Belt Conveyors
Provide flexibility for facilities that frequently change production layouts or product types.
Selecting the appropriate conveyor type ensures smooth product movement and long-term operational efficiency.
Advantages of Industrial Conveyor Automation
Automated material handling offers several practical benefits.
Increased Productivity
Continuous product movement minimizes delays between manufacturing stages.
Improved Product Safety
Controlled transportation reduces the risk of product damage during handling.
Lower Operating Costs
Automation reduces dependence on manual labor while improving resource utilization.
Better Workplace Safety
Employees spend less time lifting and transporting heavy materials manually.
Consistent Production Flow
Products move through the facility at controlled speeds, supporting stable production schedules.
Industries Using Material Handling Conveyors
Industrial conveyor systems support numerous sectors, including:
- Automotive manufacturing
- Food processing
- Pharmaceutical production
- FMCG industries
- Warehousing and logistics
- Packaging companies
- Textile manufacturing
- Engineering industries
- Chemical processing
- Airport infrastructure
Each application requires customized engineering to match operational requirements.
Factors to Evaluate Before Choosing a Solution
Before investing in a conveyor system, businesses should assess:
- Production capacity
- Product dimensions and weight
- Factory layout
- Available floor space
- Future expansion plans
- Automation integration requirements
- Maintenance accessibility
These considerations help ensure the system delivers reliable performance throughout its operational life.
Why Custom Engineering Delivers Better Results
Every manufacturing facility has unique workflows, production targets, and space constraints. Standard conveyor systems may not fully address these requirements.
Customized material handling solutions can improve:
- Production line efficiency
- Warehouse organization
- Loading and unloading operations
- Product tracking
- Equipment integration
- Overall operational flexibility
Engineering solutions tailored to the production environment typically provide better long-term value.
Investing in Smarter Manufacturing Infrastructure
Industrial automation continues transforming manufacturing facilities across India. Conveyor systems now serve as the foundation for efficient material movement, helping businesses increase productivity while maintaining consistent quality standards.
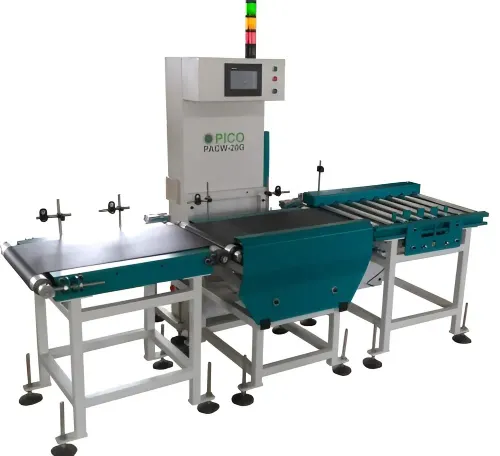
Companies exploring Industrial Material Handling Conveyor Solutions frequently work with engineering specialists such as Pico Automation, which develops customized conveyor and automation systems for manufacturing, warehousing, logistics, and industrial applications. Partnering with an experienced provider helps businesses build scalable material handling infrastructure that supports operational excellence and future business expansion.
Keywords