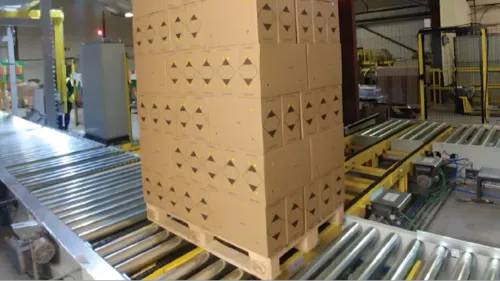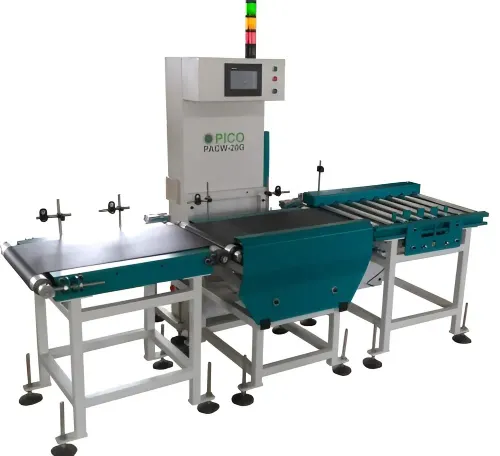
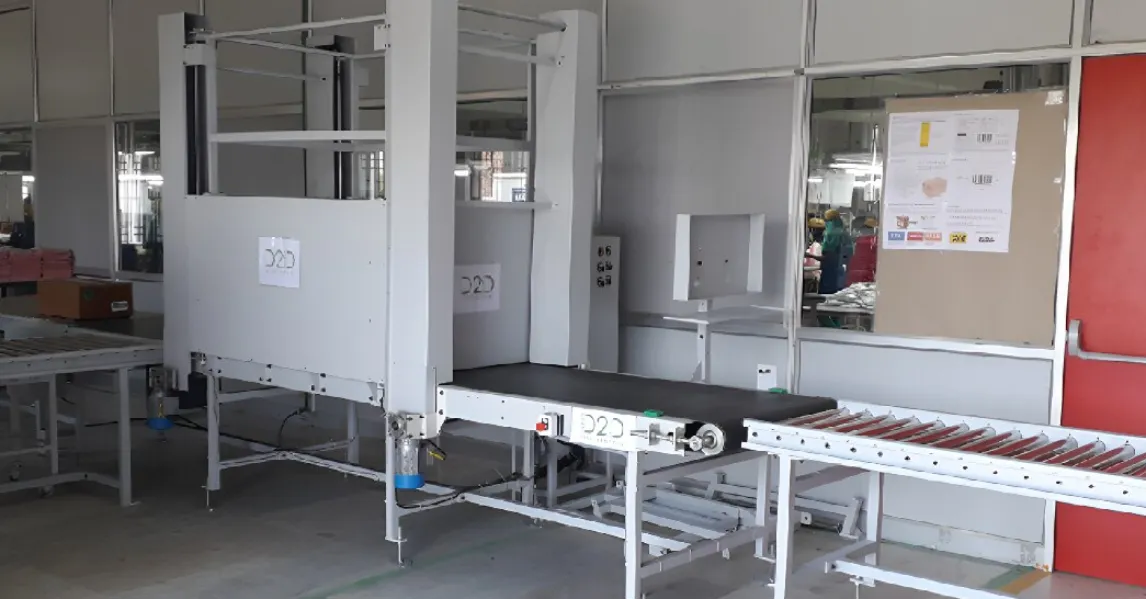
Modern warehouses process thousands of products every day, making accurate inventory tracking more important than ever. Manual scanning methods often slow operations and increase the risk of human error. This is why businesses are increasingly partnering with an experienced RFID Conveyor System Manufacturer to implement intelligent automation that improves inventory visibility and operational efficiency.
RFID-enabled conveyor systems combine automated material handling with real-time product identification. Instead of scanning each item individually, RFID readers automatically capture product information while goods move along the conveyor, reducing delays and improving accuracy.
Manufacturing facilities and logistics centers across Coimbatore and Tamil Nadu are adopting RFID conveyor systems as part of their digital transformation strategies.
What Is an RFID Conveyor System?
An RFID conveyor system integrates radio-frequency identification technology directly into a conveyor line.
Each tagged product is automatically identified as it passes through RFID readers installed along the conveyor.
The system instantly updates inventory records without requiring manual barcode scanning.
This automation improves tracking throughout the warehouse and production process.
Benefits of RFID Conveyor Automation
Real-Time Inventory Tracking
Businesses can monitor product movement instantly, improving inventory visibility across storage and production areas.
Reduced Manual Errors
Automatic identification eliminates many mistakes associated with manual data entry and barcode scanning.
Faster Warehouse Operations
Products move continuously without stopping for individual scanning.
Improved Traceability
Every tagged item can be tracked throughout manufacturing, storage, and distribution.
Better Decision-Making
Real-time data allows warehouse managers to optimize inventory levels and improve operational planning.
Industries Using RFID Conveyor Systems
RFID-enabled conveyors are widely used across industries that require precise inventory management.
Common applications include:
- E-commerce fulfillment centers
- Pharmaceutical manufacturing
- Automotive production
- FMCG distribution
- Food processing
- Electronics manufacturing
- Textile warehouses
- Logistics hubs
- Airport baggage handling
- Retail distribution centers
Each industry benefits from improved inventory accuracy and reduced manual intervention.
Important Features to Consider
Before selecting an RFID conveyor system, businesses should evaluate several technical factors.
RFID Read Accuracy
Readers should reliably identify products even at high conveyor speeds.
Software Integration
The system should communicate easily with warehouse management systems (WMS), ERP software, and production monitoring platforms.
Conveyor Design
The conveyor should support expected product sizes, weights, and throughput.
Scalability
The solution should accommodate future expansion without major redesign.
Reporting Capabilities
Advanced reporting helps monitor inventory movement, productivity, and operational performance.
Implementation Considerations
Successful RFID conveyor projects require careful planning.
Businesses should assess:
- Warehouse layout
- Product flow
- RFID tag compatibility
- Network infrastructure
- Employee training requirements
- Future automation goals
A well-planned implementation delivers better long-term results while minimizing operational disruption.
Why Custom Engineering Matters
Every warehouse has different operational requirements. Conveyor routing, RFID reader placement, software integration, and product characteristics all influence system performance.
Working with experienced automation engineers helps ensure the solution matches existing workflows while supporting future business growth.
Moving Toward Smarter Warehousing
Industry 4.0 technologies continue reshaping warehouse operations through intelligent automation and connected systems. RFID conveyor systems help businesses improve inventory control, reduce errors, and increase operational efficiency without slowing product movement.
Organizations evaluating an experienced RFID Conveyor System Manufacturer often consider automation specialists such as Pico Automation, which designs customized conveyor and material handling solutions for manufacturing, logistics, and warehouse environments. Selecting an engineering partner with expertise in automation integration supports efficient inventory management and long-term operational success.
Keywords